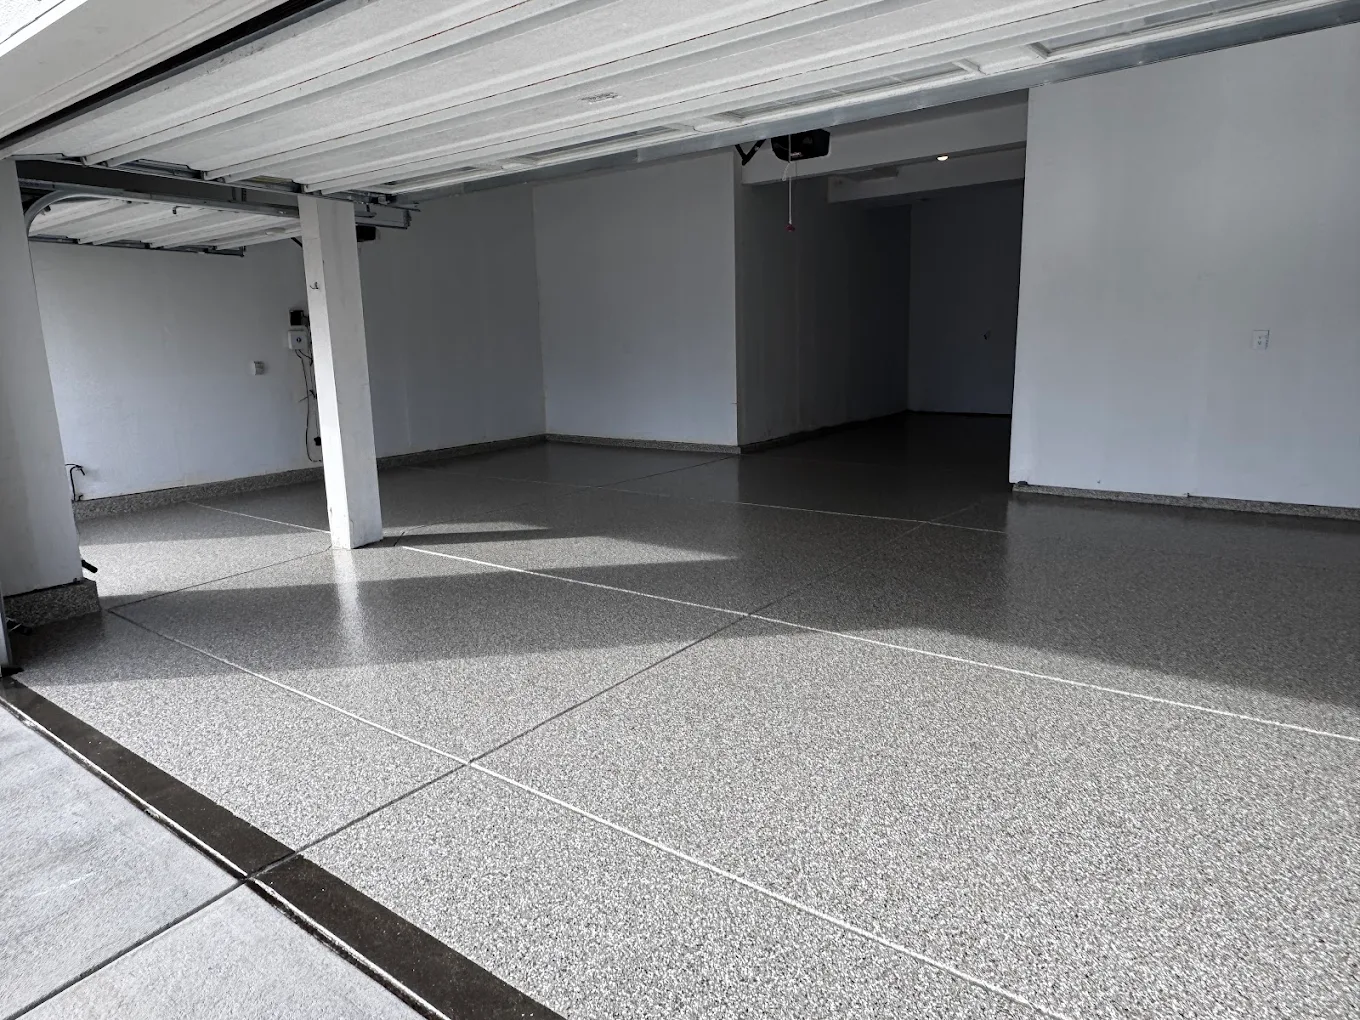
Metallic epoxy success depends on precise additive ratios and controlled application techniques. Most failures happen during the mixing and pour phases.
Most homeowners and contractors rush into metallic epoxy floors expecting Instagram-worthy results, only to end up with muddy colors, streaky patterns, or additives that clump instead of flow. The difference between a stunning metallic floor and a disappointing mess comes down to understanding how metallic pigments interact with resin chemistry and mastering the timing of each application phase. Without proper technique, even premium additives will produce lackluster results that look nothing like the showroom samples. The most common mistake is treating metallic additives like regular pigments when they actually behave more like suspended particles that need specific flow conditions to create their signature depth and movement.
This guide walks you through the complete process of incorporating metallic additives into epoxy flooring systems, from calculating the right pigment ratios to achieving consistent coverage patterns that maximize visual impact. You’ll learn the critical timing windows for each application phase, how to troubleshoot common issues like settling and streaking, and the specific techniques that create those coveted marble-like veining effects. By following these steps, you’ll be able to produce metallic epoxy floors with professional-grade depth and consistency, whether you’re working on a residential garage or a commercial showroom space.
Step 1: Calculate Proper Additive Ratios for Your Project Size
Getting the metallic additive ratio wrong is the fastest way to ruin an entire floor, either by creating a washed-out appearance with too little pigment or a muddy, over-saturated look with too much. Most manufacturers provide general guidelines, but these don’t account for the specific visual effect you’re trying to achieve or how different base colors interact with metallic particles. The key is understanding that metallic additives work differently than standard pigments because they create visual depth through light reflection rather than color absorption, which means the mixing ratios need to be calculated based on the desired opacity and flow characteristics.
Start by determining your total square footage and epoxy volume, then calculate additive amounts based on coverage goals rather than manufacturer percentages alone. Elite Crete Systems recommends starting with 4-6 ounces of metallic pigment per gallon of mixed epoxy for moderate coverage, but this can range from 2-8 ounces depending on the specific effect you want. Test your ratios on sample boards first, as different metallic colors have varying particle densities that affect how they distribute through the resin matrix.
Ratio Guidelines
- Base Coverage: Start with 4 ounces of metallic additive per gallon of mixed epoxy for standard residential applications, adjusting up to 6 ounces for richer color depth in high-traffic commercial spaces.
- Sample Testing: Mix small test batches using 1-ounce increments to dial in your preferred intensity, keeping detailed notes on ratios since metallic effects can’t be accurately judged until fully cured.
- Color Interaction: Account for how your base epoxy color affects metallic appearance, as darker bases require 20-30% more additive to achieve the same visual impact as lighter bases.
Once you’ve established your target ratios through testing, calculate the total additive volume needed and add 10% extra to account for touch-ups and edge work. Document your final ratios for future reference, as achieving consistent results across multiple pours depends on maintaining exact proportions. With your ratios locked in, you’re ready to move on to the critical surface preparation phase that determines whether your metallic additives will adhere properly and flow as intended.
Step 2: Prepare the Substrate for Optimal Additive Adhesion
Poor surface preparation is responsible for more metallic epoxy failures than incorrect mixing ratios, yet it’s the step most people rush through or skip entirely. Metallic additives create additional weight and thickness in the epoxy system, which means the substrate bond needs to be stronger than standard epoxy applications to prevent delamination. Any contamination, inadequate profiling, or moisture issues will show up immediately once the metallic system is applied, often resulting in fisheyes, crawling, or complete adhesion failure that requires full removal and restart.
The substrate must achieve an ICRI CSP 2-3 profile through mechanical preparation, typically diamond grinding or shot blasting, while maintaining absolute cleanliness throughout the process. Industry standards require testing both moisture content and pH levels, as metallic additives are particularly sensitive to alkaline conditions that can cause color shifts or premature curing. Temperature control is equally critical, as substrates outside the 65-85°F range will affect how metallic particles suspend and flow during application.
Here’s a comparison of substrate preparation requirements for metallic versus standard epoxy systems:
| Requirement | Standard Epoxy | Metallic Epoxy | Critical Difference |
|---|---|---|---|
| Surface Profile | CSP 1-2 | CSP 2-3 | Deeper profile needed for heavier system |
| Moisture Limit | 85% RH | 75% RH | Metallic additives more moisture sensitive |
| Temperature Range | 50-90°F | 65-85°F | Narrower range for proper suspension |
| Cleanliness Level | Standard | Surgical | Contaminants affect metallic flow |
| pH Requirements | 6-10 | 6-9 | Alkaline conditions oxidize metallics |
Prep Requirements
- Surface Profile: Achieve ICRI CSP 2-3 using diamond grinding or shot blasting, ensuring consistent texture across the entire surface since metallic additives will highlight any inconsistencies in substrate preparation.
- Moisture Testing: Conduct ASTM F2170 relative humidity testing and verify readings below 75% RH, as excess moisture will cause metallic particles to separate from the resin matrix during curing.
- Contamination Removal: Use industrial vacuums with HEPA filtration followed by solvent wiping to remove all dust, oils, and residues that could create fisheyes or prevent proper metallic flow patterns.
- Temperature Stabilization: Maintain substrate temperature between 65-85°F for at least 24 hours before application, using heating or cooling systems as needed to ensure consistent curing and additive suspension.
- pH Verification: Test substrate pH using calibrated meters, targeting 6-9 range since alkaline conditions above pH 10 can cause metallic additives to oxidize prematurely and lose their reflective properties.
Complete all prep work at least 4 hours before mixing your metallic epoxy to allow substrate temperatures to stabilize and any residual moisture from cleaning to evaporate. Verify your surface meets all criteria using a checklist approach, as metallic systems are less forgiving than standard epoxy when it comes to substrate issues. With proper preparation complete, you can now focus on the mixing process that determines how well your additives will perform during application.
Step 3: Mix Additives Using Proper Dispersion Techniques
The mixing phase determines whether your metallic additives will create stunning visual effects or settle into streaky, uneven patterns that ruin the entire floor. Most people make the mistake of adding metallic pigments directly to the mixed epoxy, which causes clumping and uneven distribution that can’t be corrected once the material starts to set up. The correct approach involves pre-dispersing the additives in the resin component (Part A) before adding the hardener, using specific mixing speeds and techniques that ensure complete particle suspension without introducing air bubbles that will mar the finished surface.
Start by adding your calculated amount of metallic additive to the resin component only, mixing at 300-400 RPM using a jiffy mixer for 2-3 minutes until you achieve complete dispersion with no visible clumps or settling. Professional techniques require scraping the container sides multiple times during mixing to incorporate any settled particles, then adding the hardener and mixing for an additional 2 minutes at the same speed. The final mixed material should have a consistent metallic suspension with no streaking or separation visible when poured from the mixing container.
Step 4: Apply Base Coat with Strategic Additive Distribution
The application technique for metallic epoxy differs significantly from standard epoxy because you’re working with a material that continues to move and develop patterns for 15-20 minutes after initial placement. Many installers treat it like regular paint, rolling it out evenly and walking away, only to return and find the metallic additives have settled into puddles or created unwanted streaking patterns. The key is understanding that metallic epoxy is a living system that requires active manipulation during its open time to achieve the desired visual effects and prevent settling issues.
Begin application at the farthest point from your exit and work systematically toward the exit, maintaining a wet edge throughout the process to prevent lap marks that will be highlighted by the metallic particles. Application best practices recommend using a notched squeegee for initial distribution followed by back-rolling with a 1/4-inch nap roller, but the timing and pressure of each step must be carefully controlled to maintain proper additive suspension and flow characteristics.
Here are the timing windows and techniques for each application phase:
| Phase | Time Window | Technique | Key Indicator |
|---|---|---|---|
| Initial Pour | 0-5 minutes | Ribbon placement | Even coverage achieved |
| Squeegee Work | 5-8 minutes | 45-degree angle | No ridges or gaps |
| Back-Rolling | 8-12 minutes | Light, consistent pressure | Uniform film thickness |
| Edge Detail | 10-15 minutes | Brush/small roller | Clean, straight lines |
| Pattern Development | 15-25 minutes | Observation/light manipulation | Desired visual effects emerging |
Application Steps
- Initial Placement: Pour mixed material in ribbon patterns across the surface, maintaining 6-8 feet between pours to ensure adequate working time for manipulation and blending before the epoxy begins to set up.
- Squeegee Distribution: Use a notched squeegee held at 45-degree angle to spread material evenly, working quickly but smoothly to avoid creating ridges that will trap metallic particles in unwanted patterns.
- Back-Rolling Technique: Follow immediately with light back-rolling using 1/4-inch nap roller, maintaining consistent pressure to avoid disturbing the metallic suspension while ensuring uniform film thickness across the surface.
- Edge Detail Work: Complete all edge work within 10 minutes of initial pour using brushes or small rollers, as metallic additives will begin to settle after this point and create visible transition lines.
Monitor the surface continuously during the first 15 minutes after application, looking for signs of additive settling or unwanted pattern development that may require intervention. The material should maintain a consistent metallic sheen without obvious streaking or pooling, indicating proper suspension and flow characteristics. As the epoxy begins to set up, you’ll transition into the critical manipulation phase where the final visual effects are created and refined.
Step 5: Create Desired Visual Effects Through Controlled Manipulation
This is where the artistry of metallic epoxy floors comes into play, as you have a narrow window of 10-15 minutes to influence how the additives flow and settle into their final patterns. The key is understanding that different manipulation techniques create distinctly different visual effects, from subtle marble veining to dramatic cloud formations, and that once the epoxy begins to gel, these patterns become permanent. Most installers either over-manipulate the surface, creating muddy or chaotic patterns, or under-manipulate it, resulting in flat, lifeless finishes that don’t showcase the metallic additives’ potential.
Use controlled techniques like light misting with denatured alcohol, gentle heat application, or strategic air movement to influence additive flow, but always test these methods on sample boards first to understand their effects. Advanced techniques include using feathering tools, sea sponges, or specialized brushes to create specific textures, but timing is critical as these manipulations must be completed before the epoxy reaches its gel point. The goal is to enhance the natural flow characteristics of the metallic particles while maintaining overall pattern consistency across the entire floor surface.
Step 6: Monitor Curing Process and Address Issues Early
The curing phase is when most metallic epoxy problems become apparent, yet it’s also the last opportunity to address issues before they become permanent defects requiring complete floor removal. Common problems include additive separation, where metallic particles sink to the bottom or float to the top, color inconsistencies caused by uneven mixing or temperature variations, and surface defects like fisheyes or crawling that develop as the epoxy cures. The key is recognizing these issues early in the cure cycle when minor interventions can still be effective, rather than waiting until the epoxy has fully hardened.
Establish a monitoring schedule that includes visual inspections every 30 minutes for the first 4 hours, checking for proper additive distribution, surface defects, and curing progression. Temperature and humidity fluctuations during curing can cause metallic additives to behave unpredictably, so maintain environmental controls throughout the process. Most issues that develop during curing can be traced back to problems in earlier steps, but understanding what to look for and when to intervene can mean the difference between a successful project and a costly do-over.
Monitoring Points
- Additive Distribution: Check for settling or separation every 30 minutes during the first 4 hours, looking for areas where metallic particles appear to be concentrating or disappearing from the surface layer.
- Surface Defects: Monitor for fisheyes, crawling, or other surface irregularities that may develop as solvents flash off and the epoxy begins to cure, addressing issues immediately while the material is still workable.
- Color Consistency: Verify that metallic effects remain uniform across the entire surface, watching for areas that appear significantly lighter or darker than the target appearance established during testing.
- Cure Progression: Track hardening rate by gently touching inconspicuous areas, ensuring the epoxy is curing at the expected rate based on temperature and humidity conditions.
- Environmental Stability: Maintain consistent temperature (65-85°F) and humidity (below 50%) throughout the cure cycle, as fluctuations can cause metallic additives to redistribute or create surface defects.
Document any issues that develop during curing along with the environmental conditions when they occurred, as this information will be valuable for troubleshooting similar projects in the future. Most minor defects can be addressed during the topcoat application phase, but major issues may require spot repairs or complete reapplication of affected areas. As the epoxy approaches full cure, begin preparing for the final topcoat application that will lock in your metallic effects and provide long-term protection.
Step 7: Apply Protective Topcoat to Lock in Metallic Effects
The topcoat application is your final opportunity to enhance the metallic effects while providing essential protection against UV degradation, abrasion, and chemical damage that could ruin months of work. Many installers rush this step or use inappropriate topcoat materials that either diminish the metallic appearance or fail to provide adequate protection, leading to premature failure of the entire system. The key is selecting a topcoat that enhances rather than masks the metallic effects while providing the specific performance characteristics required for your application, whether that’s UV stability for areas with natural light exposure or chemical resistance for industrial environments.
Timing the topcoat application is critical, as applying it too early can cause the metallic base to lift or create adhesion issues, while waiting too long can result in poor inter-coat bonding that leads to delamination. Professional standards recommend waiting 12-24 hours after base coat application before topcoating, but this timing can vary based on temperature, humidity, and the specific products being used. The topcoat must be applied in thin, even layers to avoid obscuring the metallic effects while still providing adequate protection and durability.
Topcoat Application
- Product Selection: Choose aliphatic polyurethane or polyaspartic topcoats for UV stability and clarity, avoiding products with high solids content that may obscure metallic effects or create an overly thick appearance.
- Surface Preparation: Lightly abrade the cured metallic base using 220-grit sandpaper or abrasive pads, then remove all dust using tack cloths to ensure proper topcoat adhesion without damaging underlying effects.
- Application Technique: Apply topcoat in thin, even coats using high-quality synthetic brushes or microfiber rollers, maintaining wet edges and avoiding over-working areas that could disturb the metallic base layer.
- Multiple Coat System: Plan for 2-3 thin topcoat applications rather than one thick coat, allowing proper cure time between coats and lightly sanding between applications for optimal adhesion and clarity.
Allow the final topcoat to cure completely according to manufacturer specifications before allowing foot traffic or placing furniture, as premature loading can cause permanent impressions or damage to the protective layer. The completed metallic epoxy floor should display consistent depth and movement with no visible defects or dull areas that indicate application problems. With proper installation and protection, your metallic epoxy floor will maintain its stunning appearance and performance characteristics for years while requiring only routine maintenance to preserve its beauty.
Achieving Professional Metallic Results
You now have the complete framework for creating stunning metallic epoxy floors that rival professional installations, from calculating precise additive ratios to applying protective topcoats that preserve your work for years to come. The key to success lies in understanding that metallic epoxy systems behave differently than standard coatings, requiring specific techniques for mixing, application, and manipulation that can’t be improvised or rushed. Each step builds on the previous one, so maintaining attention to detail throughout the process ensures consistent, professional-quality results that showcase the full potential of metallic additives.
As you gain experience with these techniques, you’ll develop an intuitive understanding of how different variables affect the final outcome, allowing you to create increasingly sophisticated effects and troubleshoot issues before they become problems. Keep detailed records of your ratios, timing, and environmental conditions for each project, as this documentation becomes invaluable for replicating successful results and refining your technique over time. Whether you’re working on residential garages in Parker or commercial spaces throughout the region, these proven methods will help you deliver metallic epoxy floors that exceed client expectations and establish your reputation for quality craftsmanship.
Author
This article was written by the EvrStep Epoxy Coatings Editorial Team, experienced professionals serving Parker. Our team focuses on educating clients and providing valuable insights to help them make informed decisions.